Confirm the matched burner configuration
This oilfield burner is a combustion assembly for a boiler or heater, not a flare. Select it against actual fuel properties, required heat input, furnace geometry, draft, usable firing range and the approved protection philosophy. Identify the fuel train, combustion-air arrangement, controls and auxiliaries actually offered. Dual-fuel capability, cold-weather provisions, emissions and certification require configuration-specific confirmation.
Useful process output and heated-fluid compatibility belong to the complete thermal-equipment review. Furnace matching cannot be established by flange size or a maximum input figure alone. Commissioning, operating work and maintenance require competent personnel, equipment-specific manufacturer information and approved project procedures. Never bypass safeguards or improvise ignition.
Evaluate engineering evidence before marketing claims
A capable oilfield burner unit manufacturer should turn your duty data into calculations, drawings, component selections and a clear list of assumptions. Ask the bidder to explain how the proposed package performs stable, controllable combustion for oilfield heaters, boilers and thermal-process equipment and how it is derated for the destination climate. Generic brochures are useful for orientation, but they are not a substitute for a project-specific technical proposal.
Review experience with comparable applications rather than counting unrelated installations. Useful references state the process duty, operating environment, delivery scope and year. Protect confidential end-user information, but request enough evidence to establish that the supplier understands the equipment and its interfaces.
Factory and quality-system checks
Design control
Check calculations, drawings, revisions and approval responsibilities.
Material traceability
Verify certificates, heat numbers and records for pressure-retaining or critical parts.
Assembly inspection
Use inspection checkpoints for alignment, cleanliness, torque and piping quality.
Functional testing
Agree no-load, load-simulation, alarm, shutdown and leak tests.
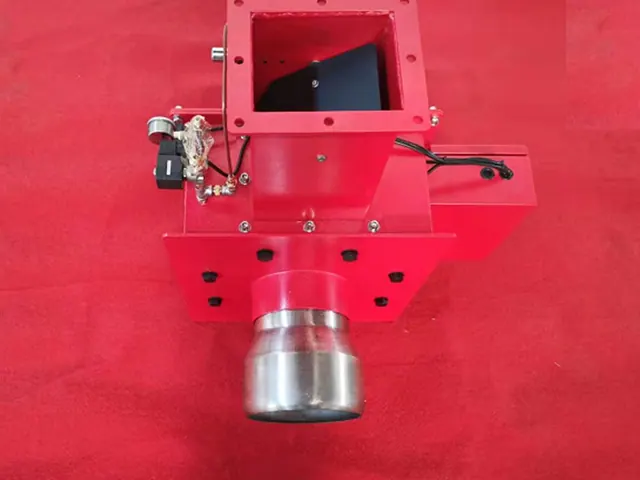
For the major assemblies—burner head and flame stabilizer, fuel train, forced-draft fan, flame safeguard and ignition controller—ask who manufactures each item, who owns the technical selection and how warranty support is coordinated. The integrator must remain accountable for the performance of the complete package.
Define the factory acceptance test in the purchase order
| FAT stage | Minimum coverage | Buyer action |
|---|---|---|
| Document review | Approved drawings, data sheets, certificates and software list | Before physical test |
| Mechanical inspection | Dimensions, access, guards, labels, piping and workmanship | Record punch items |
| Functional test | Start, stop, controls, alarms, interlocks and emergency shutdown | Witness critical sequences |
| Performance evidence | Pressure, flow, temperature, power or separation duty as applicable | State test method and tolerance |
If full-load testing is impractical at the factory, agree an alternative: component test certificates, calibrated simulation, partial-load testing and a site performance test. Acceptance criteria must be measurable, not phrases such as “runs normally.”
Documentation and support that reduce startup risk
- General arrangement, foundation and connection drawings
- Process, electrical, hydraulic and pneumatic schematics
- Operation, maintenance and troubleshooting manuals
- Parts list with manufacturer and model references
- Inspection records, calibration certificates and test reports
- Remote support, training, commissioning and warranty process
A reliable manufacturer discusses exclusions and unknowns early. Use a technical bid evaluation table to score compliance, deviations, evidence and lifecycle support before commercial negotiation.
Review the actual burner and thermal-system boundary
Request the exact offered component schedule, a written burner-to-furnace match and controlled responses to each fuel and load case. Identify the party responsible for the integrated protection and external interfaces. Component documents, enclosure ratings and familiar brands do not independently approve the assembled installation or establish unrestricted destination compliance.
Keep the accepted configuration, drawings, fuel schedule, relevant measurements and open deviations together. Review material changes to equipment or supply conditions before relying on earlier evidence. Actual commissioning, operation and maintenance require competent personnel, manufacturer information and approved project procedures.
For broader industry context, consult ASME Boiler and Pressure Vessel Code resources. Project requirements and applicable codes must still be confirmed for the destination country and end user.
Frequently asked questions
What should a qualified oilfield burner unit manufacturer provide?
Expect project calculations, drawings, component data, a deviation list, quality records, an agreed factory test and complete operation and maintenance documents.
Is a factory acceptance test necessary?
Yes. The FAT verifies workmanship, controls, alarms and agreed performance evidence before shipping, when corrections are easier and less expensive.